
Conformal Cooling Inserts
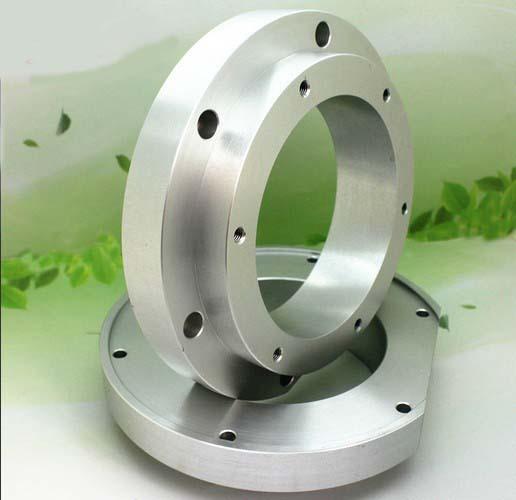
Conformal cooling inserts with channel geometries that follow the mold surface contour, reducing cycle time and improving part quality in injection molds.
| Materials | Copper, Stainless Steel |
|---|---|
| Processes | CNC Machining |
| Tolerance | ±0.01mm |
| Standard | SPI Mold Standards |
Overview
Conformal cooling inserts are precision-manufactured mold components featuring cooling channels that follow the contour of the cavity surface. Unlike conventional straight-drilled cooling lines, conformal channels maintain a consistent distance from the mold wall, delivering uniform cooling across complex part geometries. This reduces cycle times by 20–40% and significantly improves part quality by minimizing warpage, sink marks, and residual stress.
Our conformal cooling inserts are produced using a combination of 5-axis CNC machining and advanced manufacturing techniques. The channel geometry is designed based on thermal simulation of the molding process, ensuring optimal coolant flow rate and heat extraction exactly where the part needs it most.
Key Features
- Conformal channel geometry: Cooling channels follow the cavity surface contour for uniform heat extraction
- Cycle time reduction: 20–40% reduction compared to conventional straight-drilled cooling
- Improved part quality: Reduced warpage, sink marks, and residual stress from uniform cooling
- Thermal simulation: Channel layout optimized using mold flow and thermal analysis
- Material flexibility: Beryllium copper for high thermal conductivity, H13 for wear resistance, or stainless steel for corrosion resistance
- Long service life: Hardened and surface-treated for durability in production environments
Manufacturing Process
- Thermal simulation — Mold flow and thermal analysis identifies hot spots and defines the optimal channel layout
- Channel generation — Cooling channels are created using additive manufacturing or machined-in groove techniques
- 5-axis machining — Insert external geometry machined to match the mold cavity with ±0.01 mm accuracy
- Sealing and connection — Coolant inlet and outlet ports machined and sealed for leak-free operation
- Heat treatment — Hardening and tempering for wear resistance and thermal fatigue durability
- Surface treatment — Polishing or coating to suit the molding application and material being processed
- Quality inspection — CMM verification, pressure testing of cooling channels, and surface finish measurement
Specifications
| Parameter | Specification |
|---|---|
| Material | Beryllium copper (C17200), H13, SS 316L |
| Channel diameter | 3–12 mm (design dependent) |
| Channel distance from surface | 2–5 mm (part geometry dependent) |
| Thermal conductivity | BeCu: 130 W/m·K, H13: 25 W/m·K |
| Dimensional tolerance | ±0.01 mm on insert geometry |
| Coolant pressure rating | Up to 15 bar |
Applications
- Injection mold cavities with thick sections prone to warpage
- Thin-wall packaging molds requiring fast cycle times
- Medical and optical molds needing uniform cooling for stress-free parts
- Die casting inserts exposed to high thermal cycling loads
- Multi-cavity molds where balanced cooling is critical for cavity-to-cavity consistency
Request a quote for custom conformal cooling insert manufacturing.
Related Mold Manufacturing Products
- Injection Mold Cavities — Precision injection mold cavities for tooling applications
- Precision Mold Base Plates — Precision precision mold base plates for tooling applications